


READY-TO-EAT
SANITARY CONVEYING SYSTEMS FOR READY-TO-EAT FOOD PROCESSING
Sanitary conveying and handling systems engineered around your ready-to-eat products, processes and facility. From individual conveyors to complete integrated systems, PFI helps RTE processors improve food safety, product handling and production efficiency.


SANITARY BY DESIGN
Open, accessible designs and food-grade construction help make equipment easier to inspect, clean and validate—especially important for RTE products with no downstream kill step.

PRODUCT QUALITY
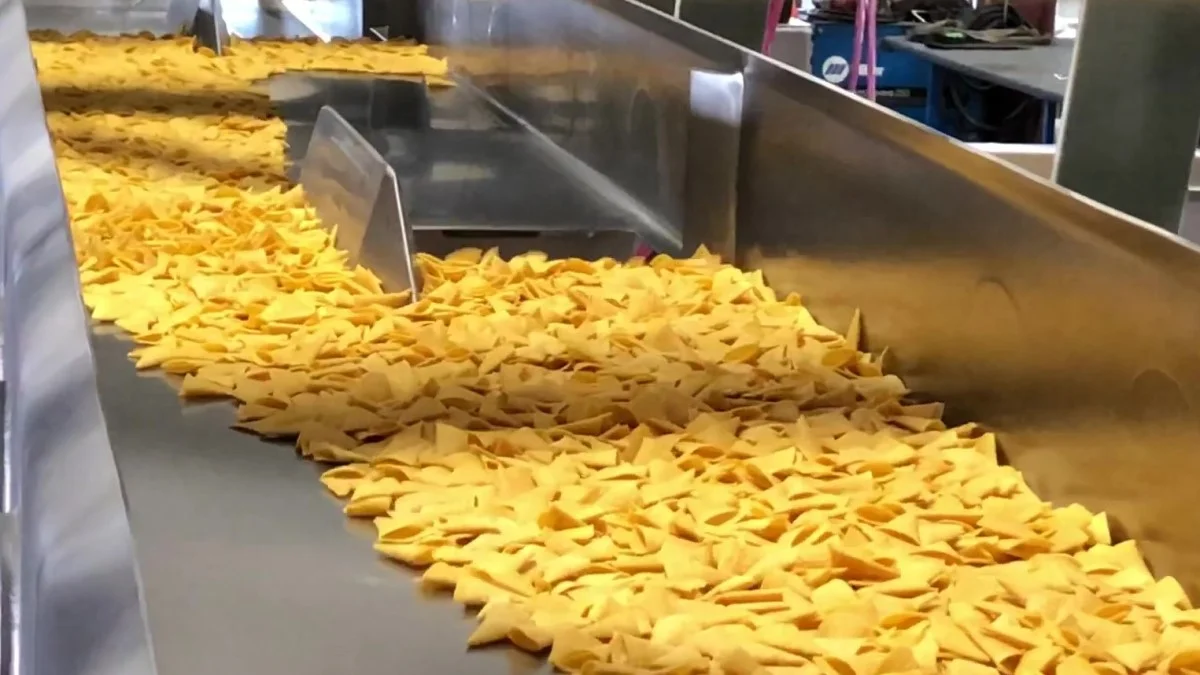
Move delicate, sticky, fresh and prepared foods gently while minimizing product damage, loss and unnecessary handling.

CUSTOM ENGINEERED
Your products, processes and plant are unique. We configure equipment and complete conveying systems around your layout, throughput, sanitation requirements and production goals.

BUILT TO INTEGRATE
We work with your team, OEMs and engineering partners to connect processing, assembly, inspection, packaging and other critical operations.
Grillo’s Pickles Expands Production with Integrated Solutions from PFI & the Grote Family of Brands

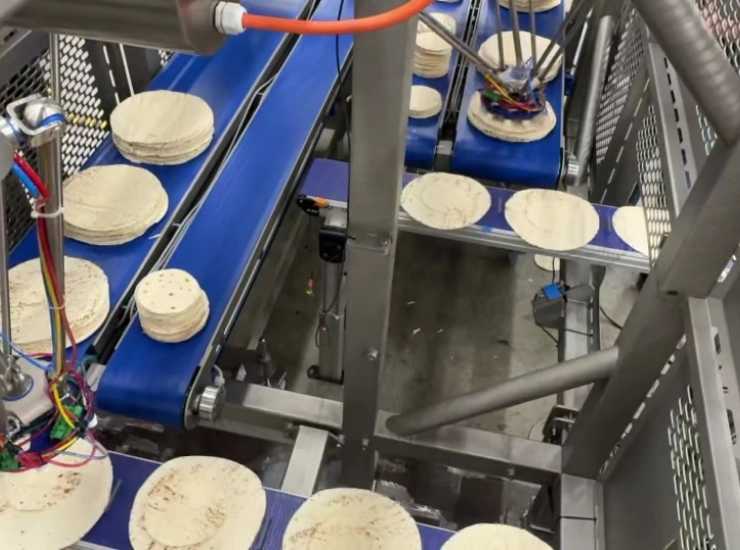
RTE production can involve everything from bulk ingredients and delicate fresh foods to assembled meals and packaged products. PFI engineers conveying solutions around your product and the requirements of each stage of production.
- Prepared meals and meal components
- Salads and salad components
- Sandwiches and wraps
- Fresh-cut fruits and vegetables
- Deli and prepared foods
- Protein and cooked ingredients
- Snack and convenience foods
- Bowls, trays and kits
CONNECT YOUR READY-TO-EAT PROCESSING LINE FROM END TO END
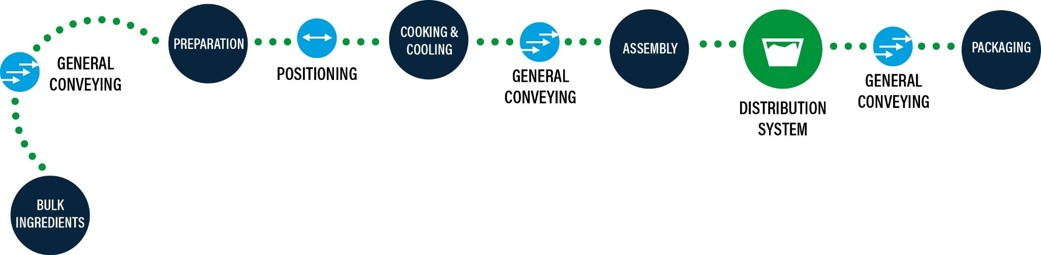
PFI engineers conveying and handling systems around your complete process—connecting your equipment, people and production steps into one efficient line. Our engineers collaborate with your team, engineering partners and other OEMs to integrate processes such as ingredient handling, preparation, cooking, cooling, assembly, inspection and packaging. The result is a system configured around your facility, product flow and production requirements.
AUTOMATION & CONTROLS
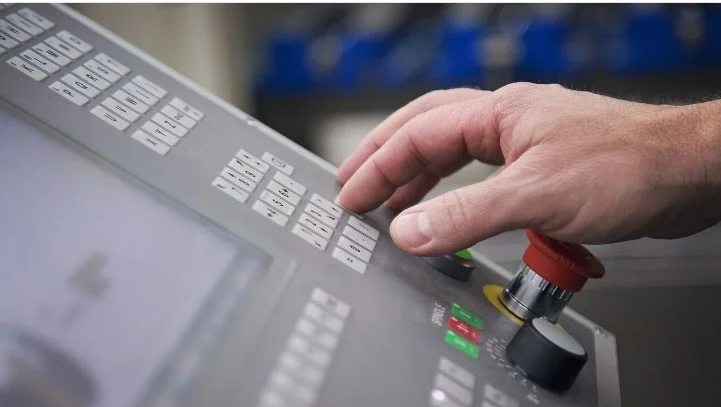
Integrate controls, sensors, inspection systems, vision, and other automation directly into your conveyance system to improve efficiency, reduce complexity, and keep production moving consistently.
Rely on us to coordinate and program controls so your equipment works together seamlessly.
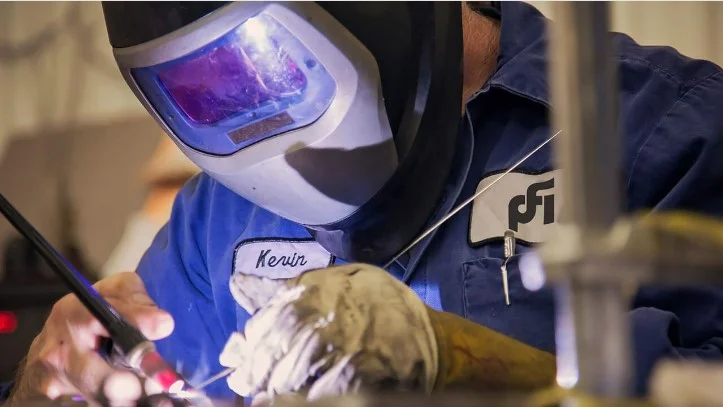
INSTALLATION, PARTS, & TECHNICAL SUPPORT
Get your operation up and running fast with installation by our skilled technicians and millwright network.
Post-install, PFI supports your equipment with OEM and replacement parts and technical services.
SANITARY CONVEYOR DESIGN FOR RTE FOOD SAFETY
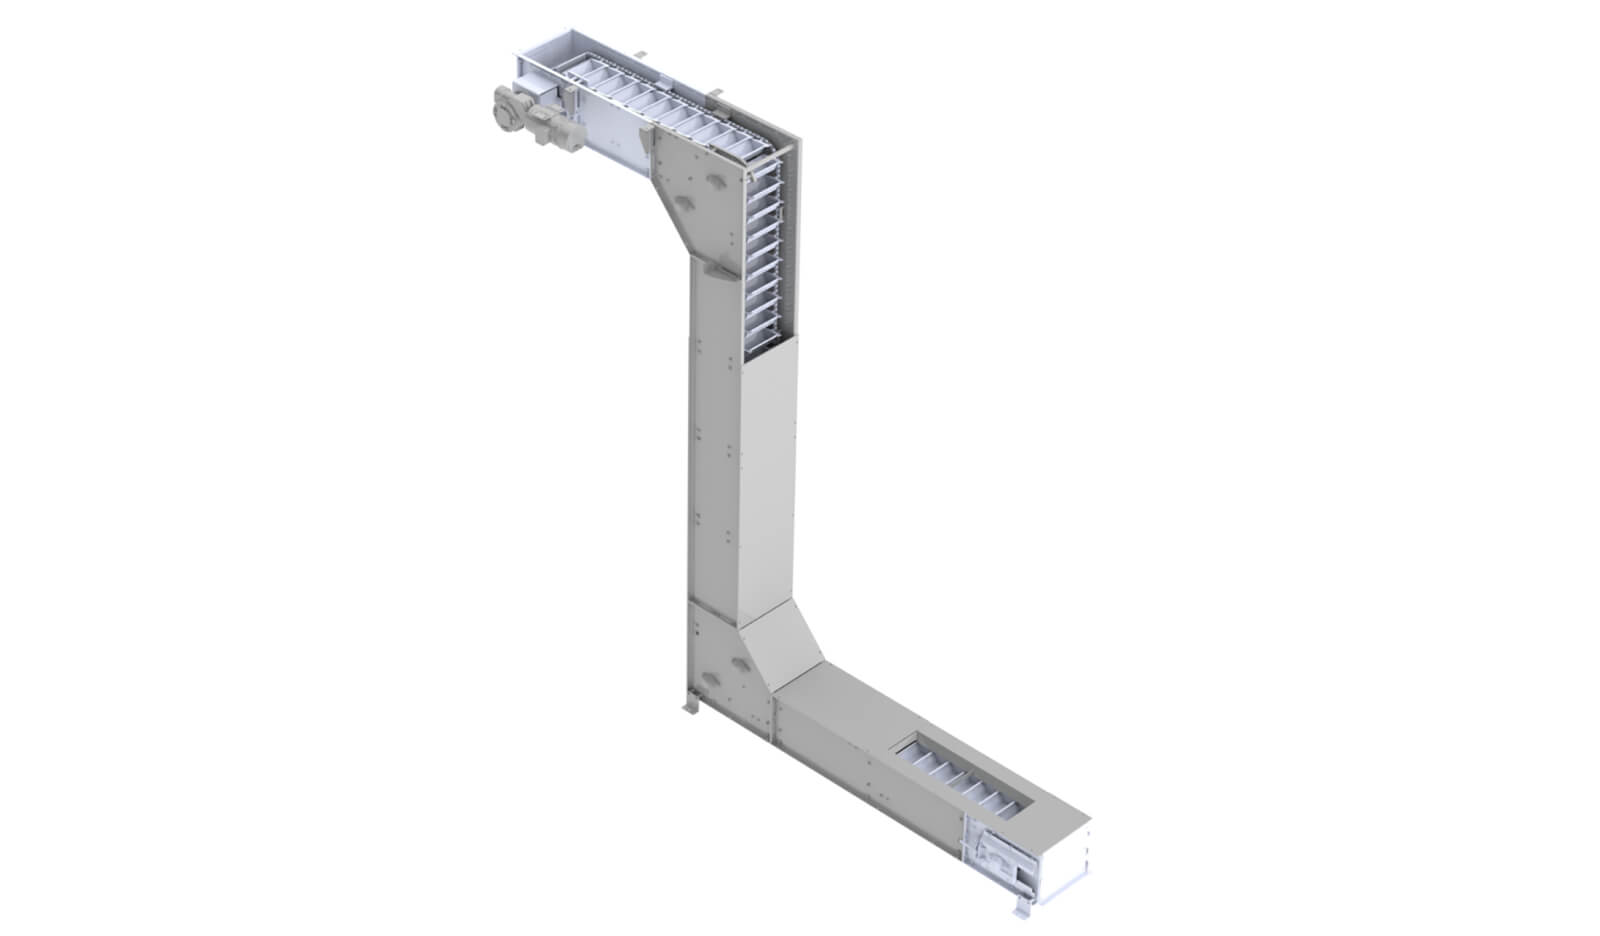
We put sanitary design first. Our equipment is designed for maximum accessibility and ease of cleaning, with stainless steel construction, open frames, reduced harborage points, simplified maintenance, food-grade materials, hygienic welds, and more.


Distribution Conveyor System
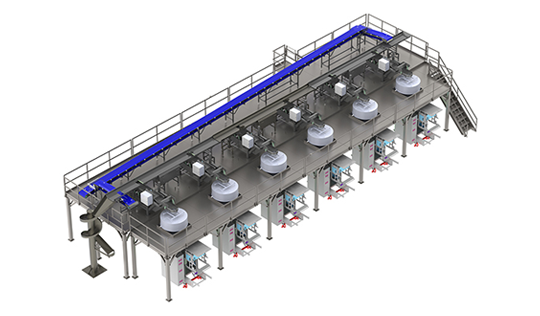
Feed multiple product streams through a system of vibratory feeders and conveying.
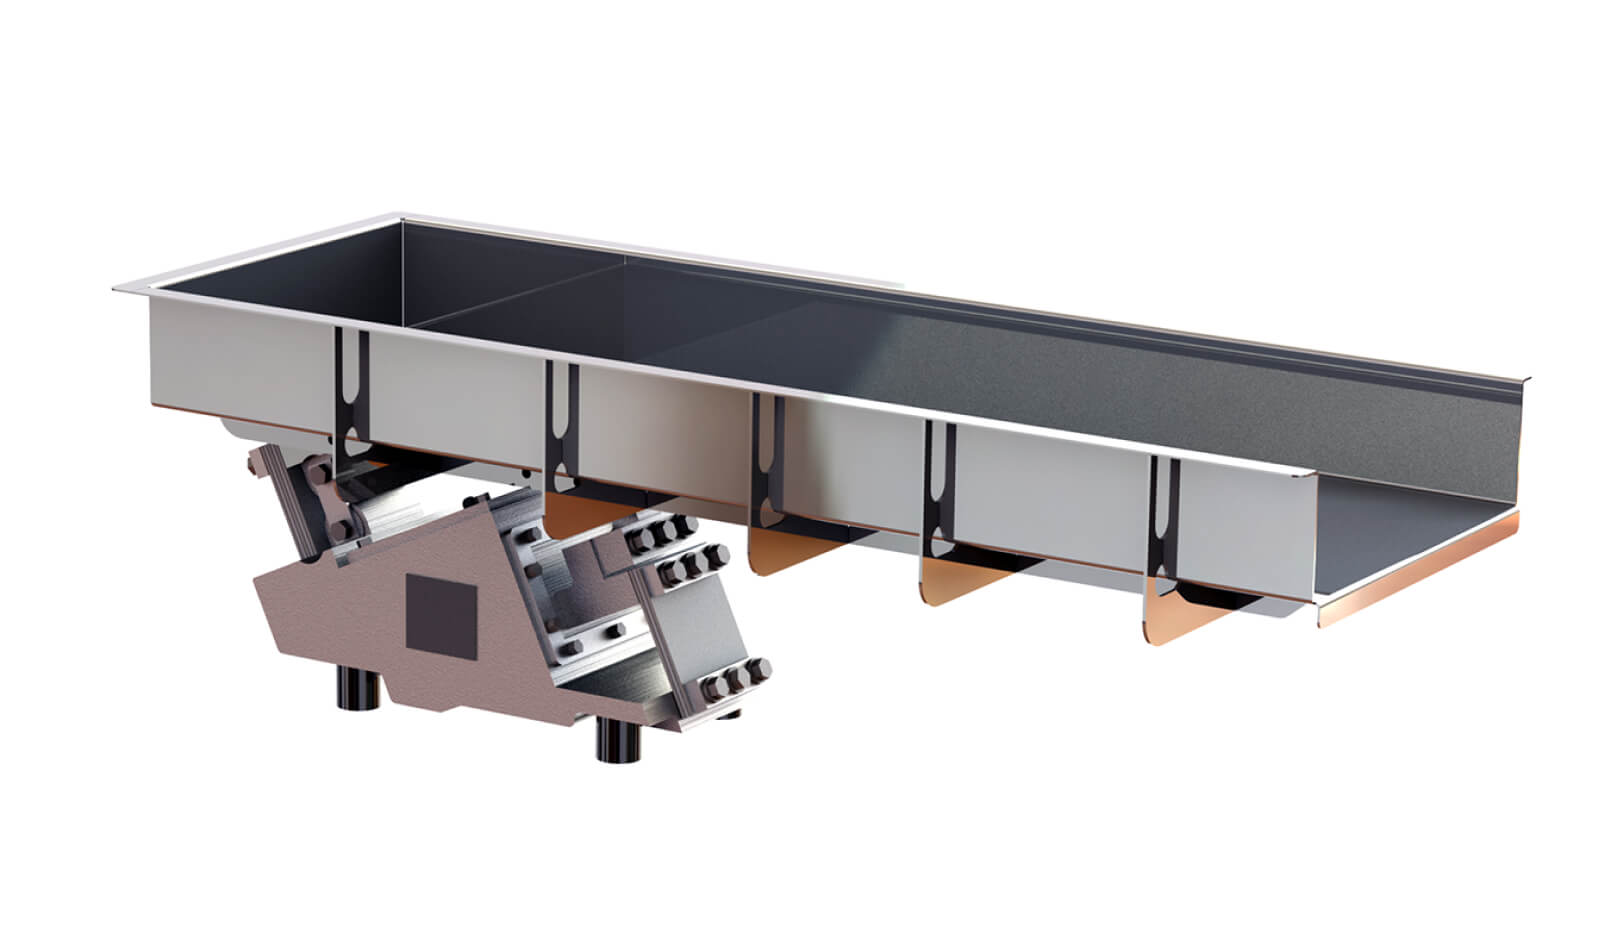
EDF Feeder
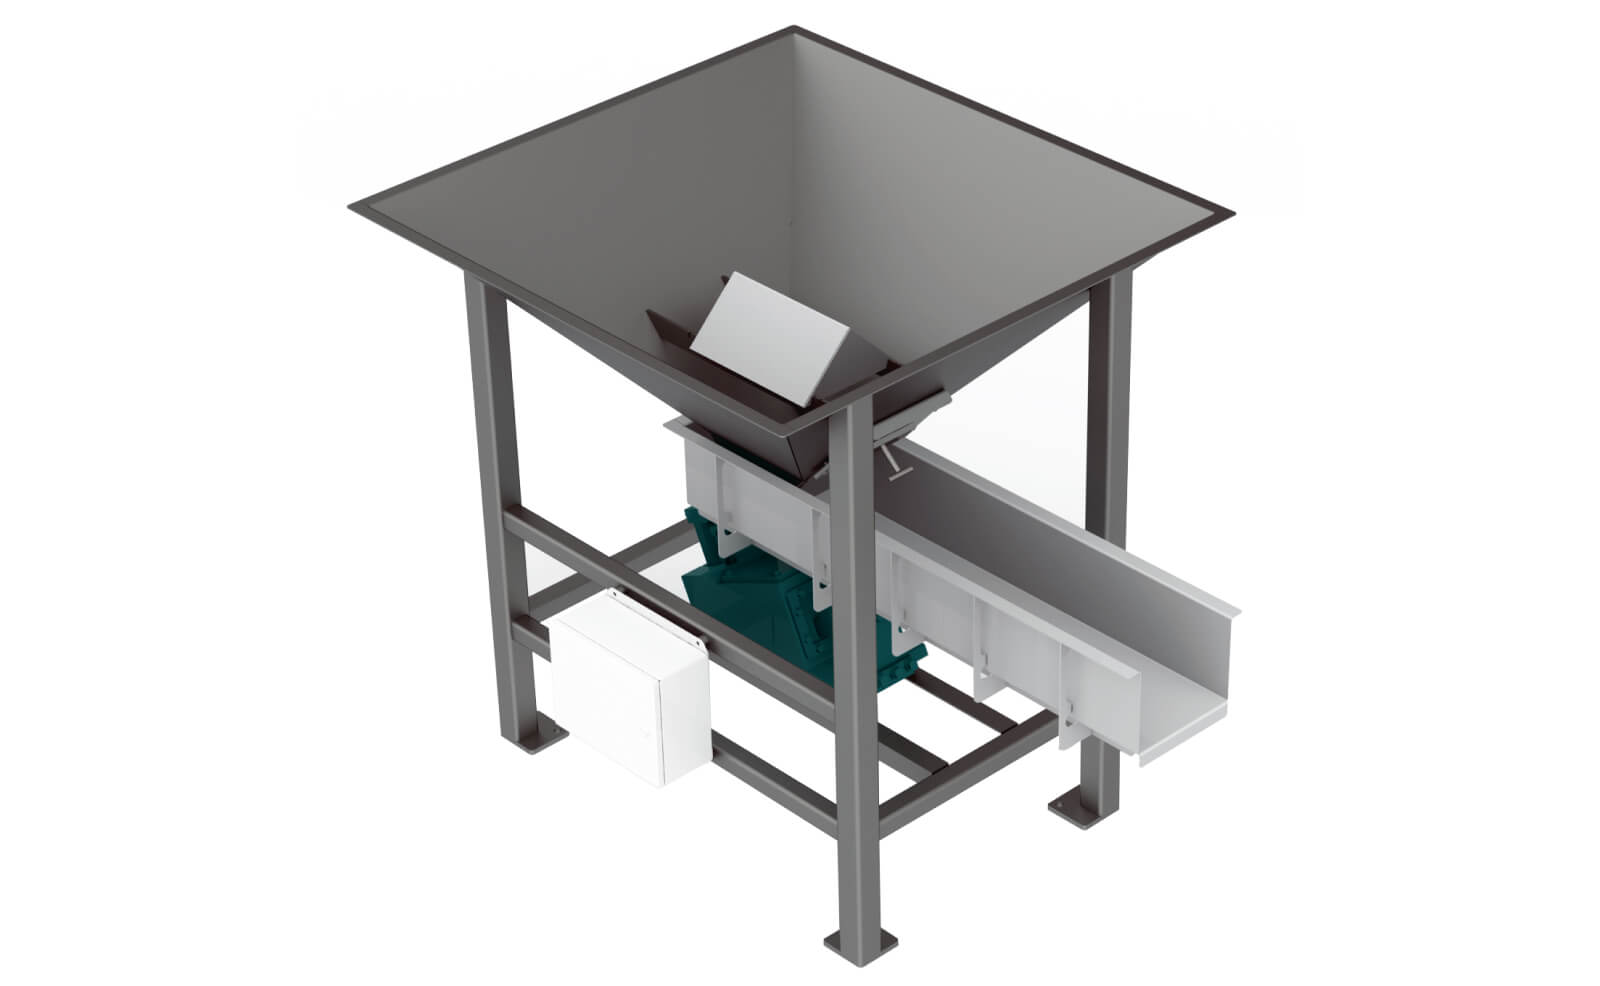
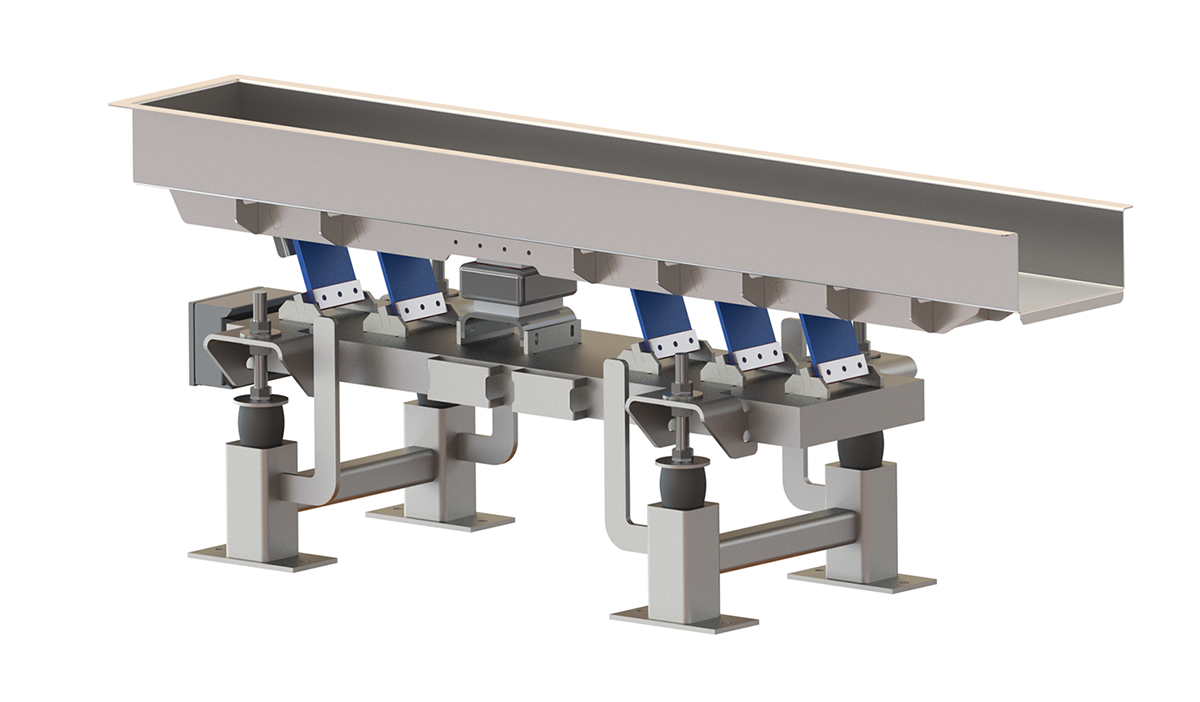
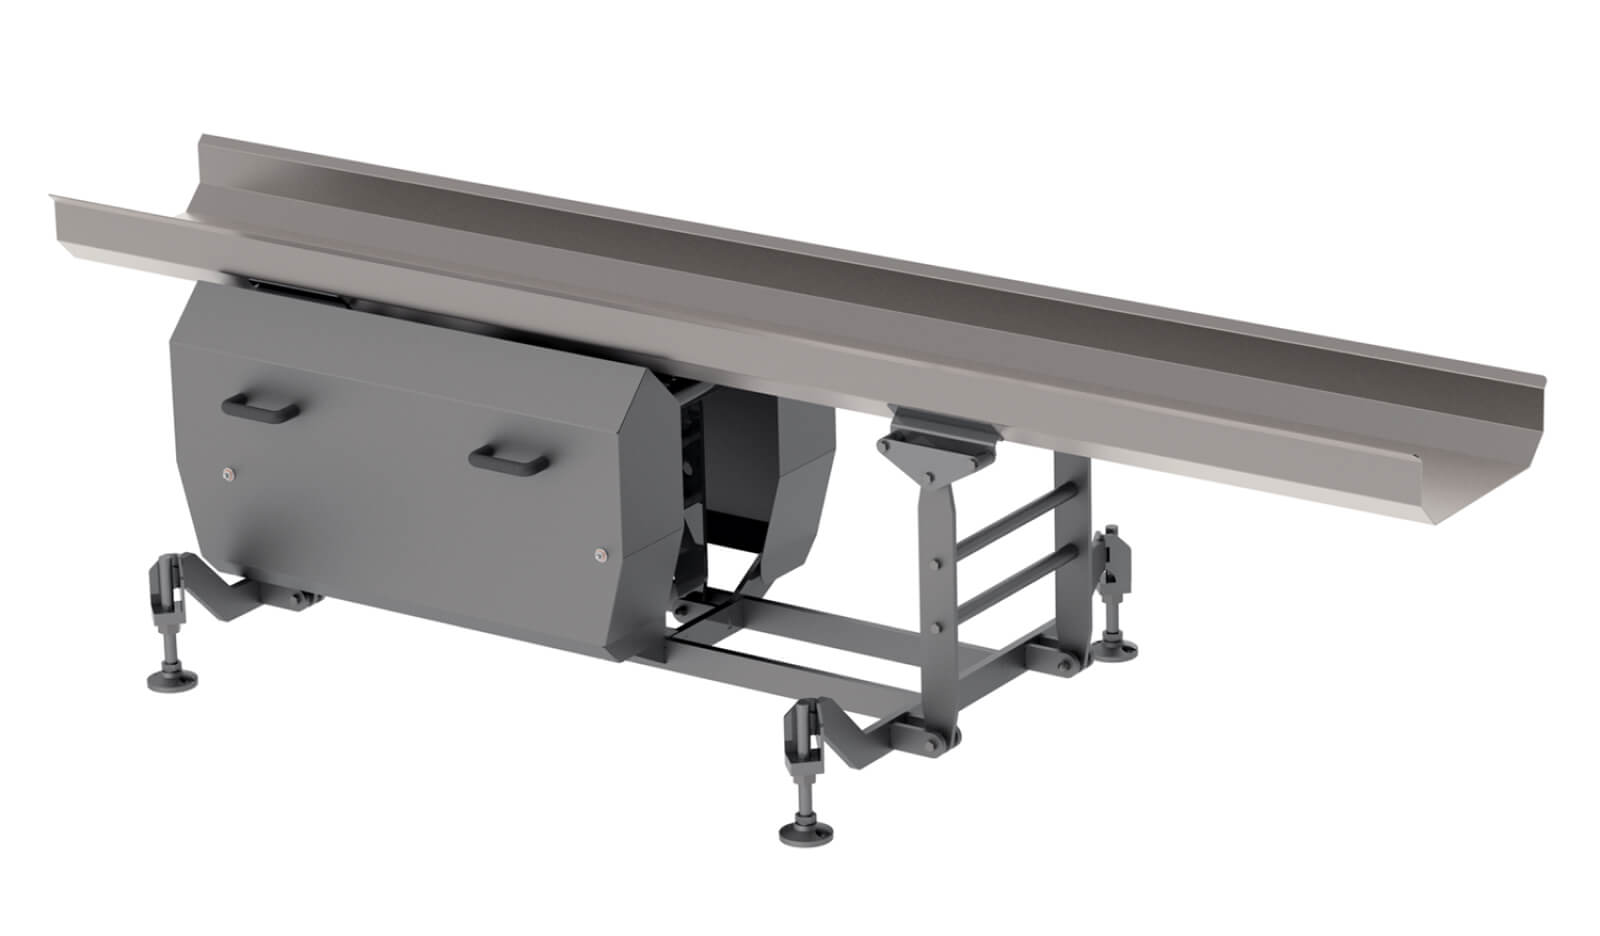
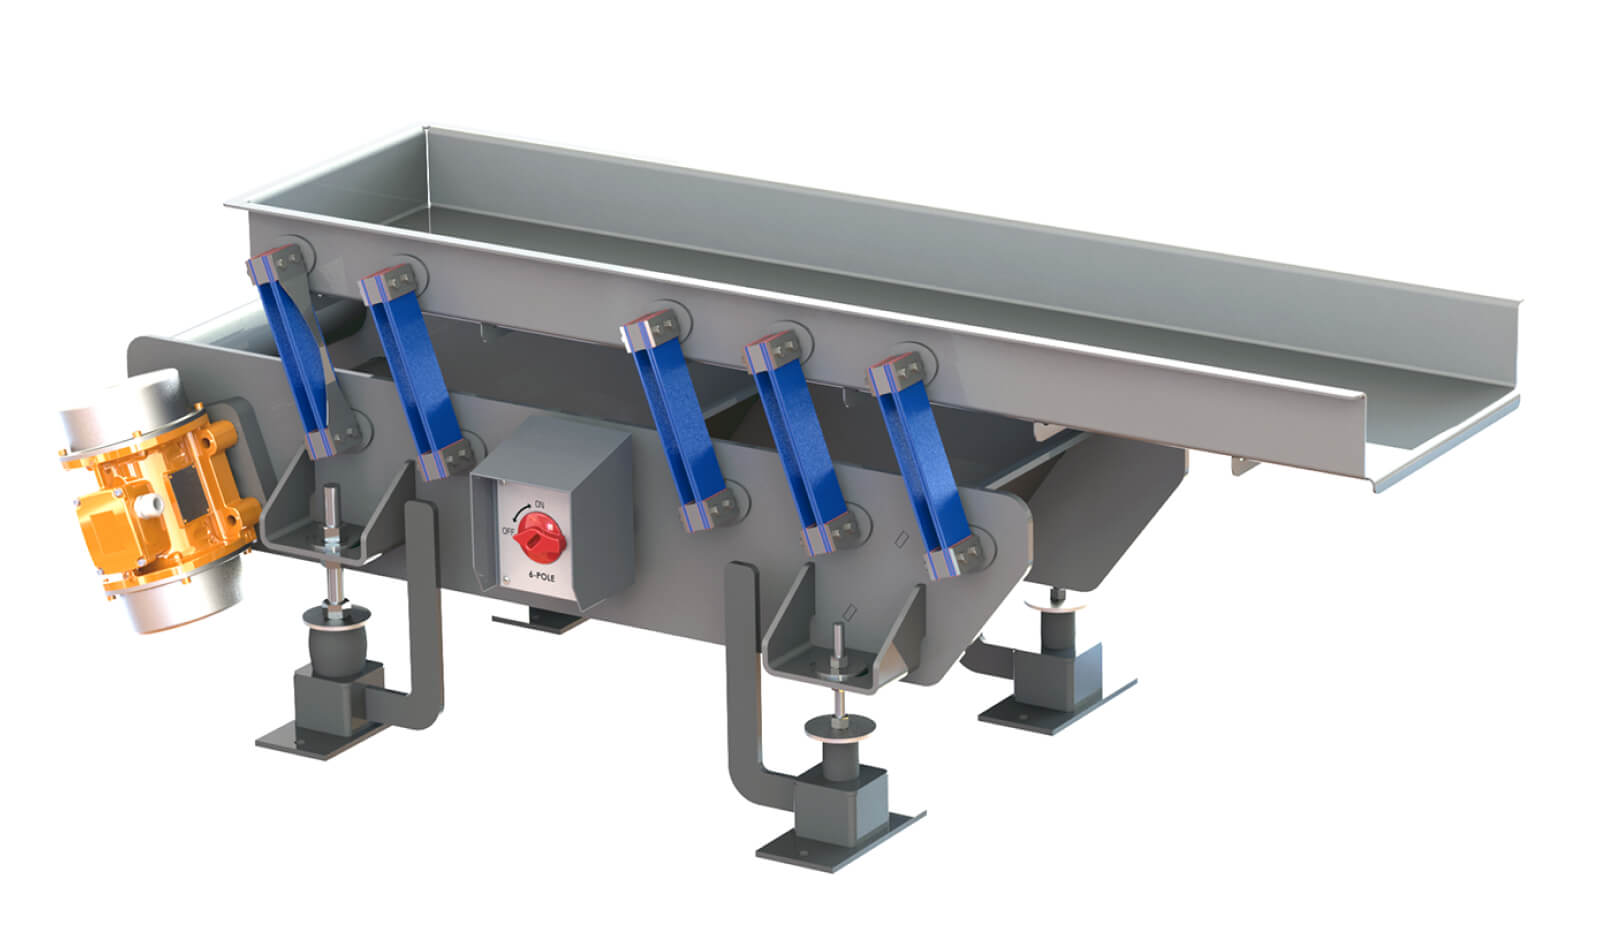
Feed, screen, and lane product accurately with this versatile vibratory feeder. Use on its own or with a Hopper Feeder or Mix-Blend System.
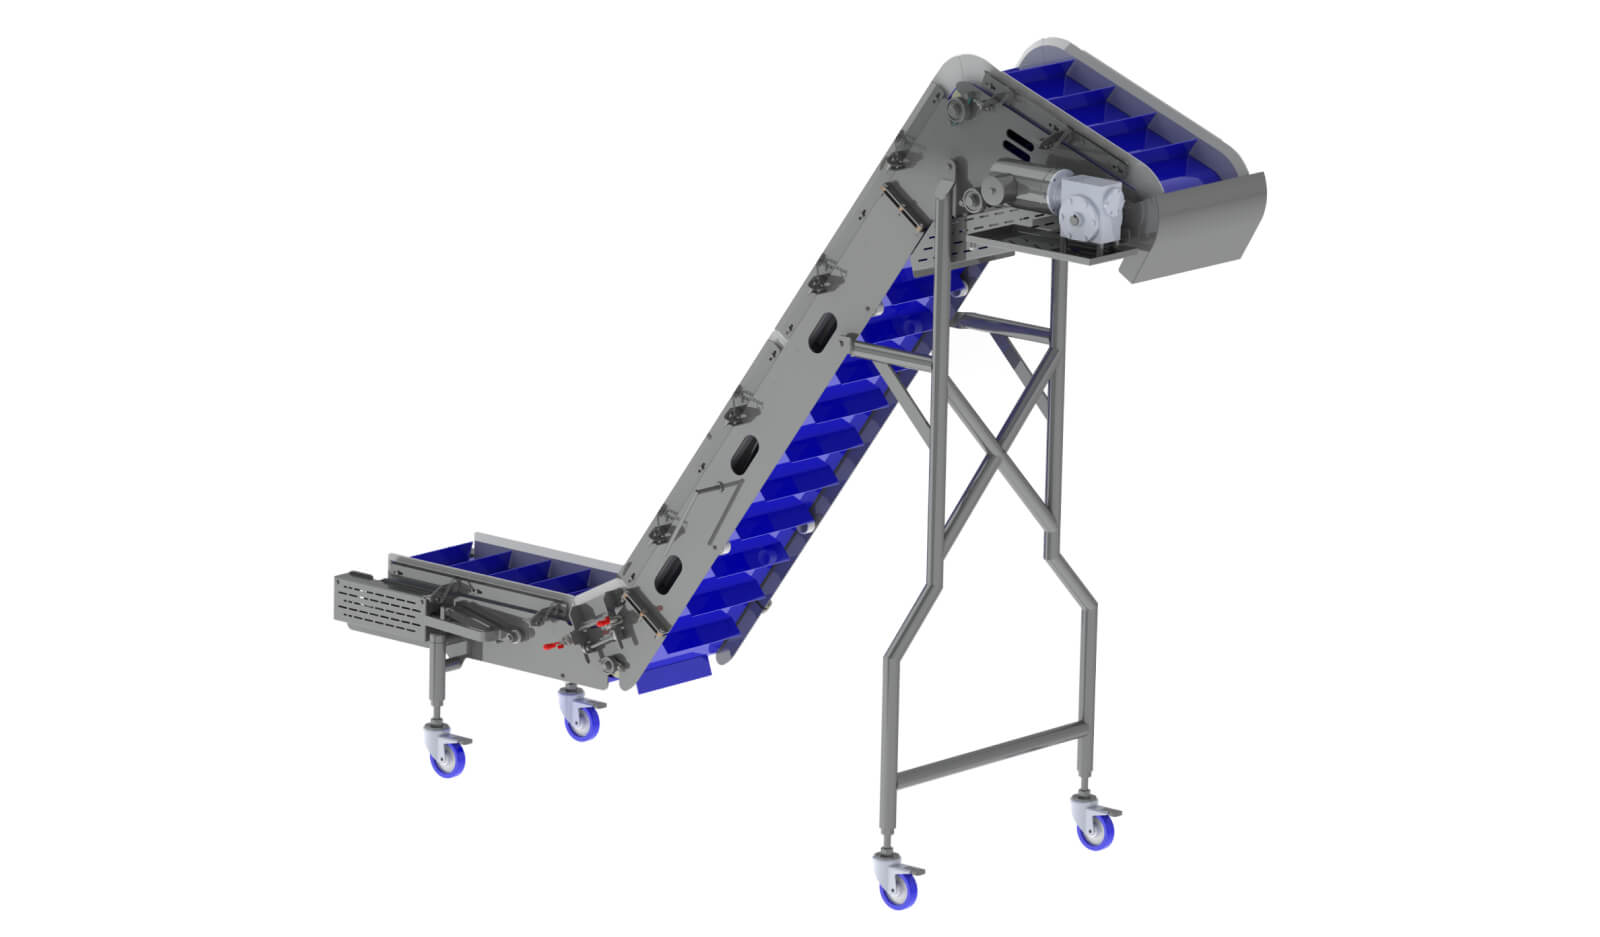
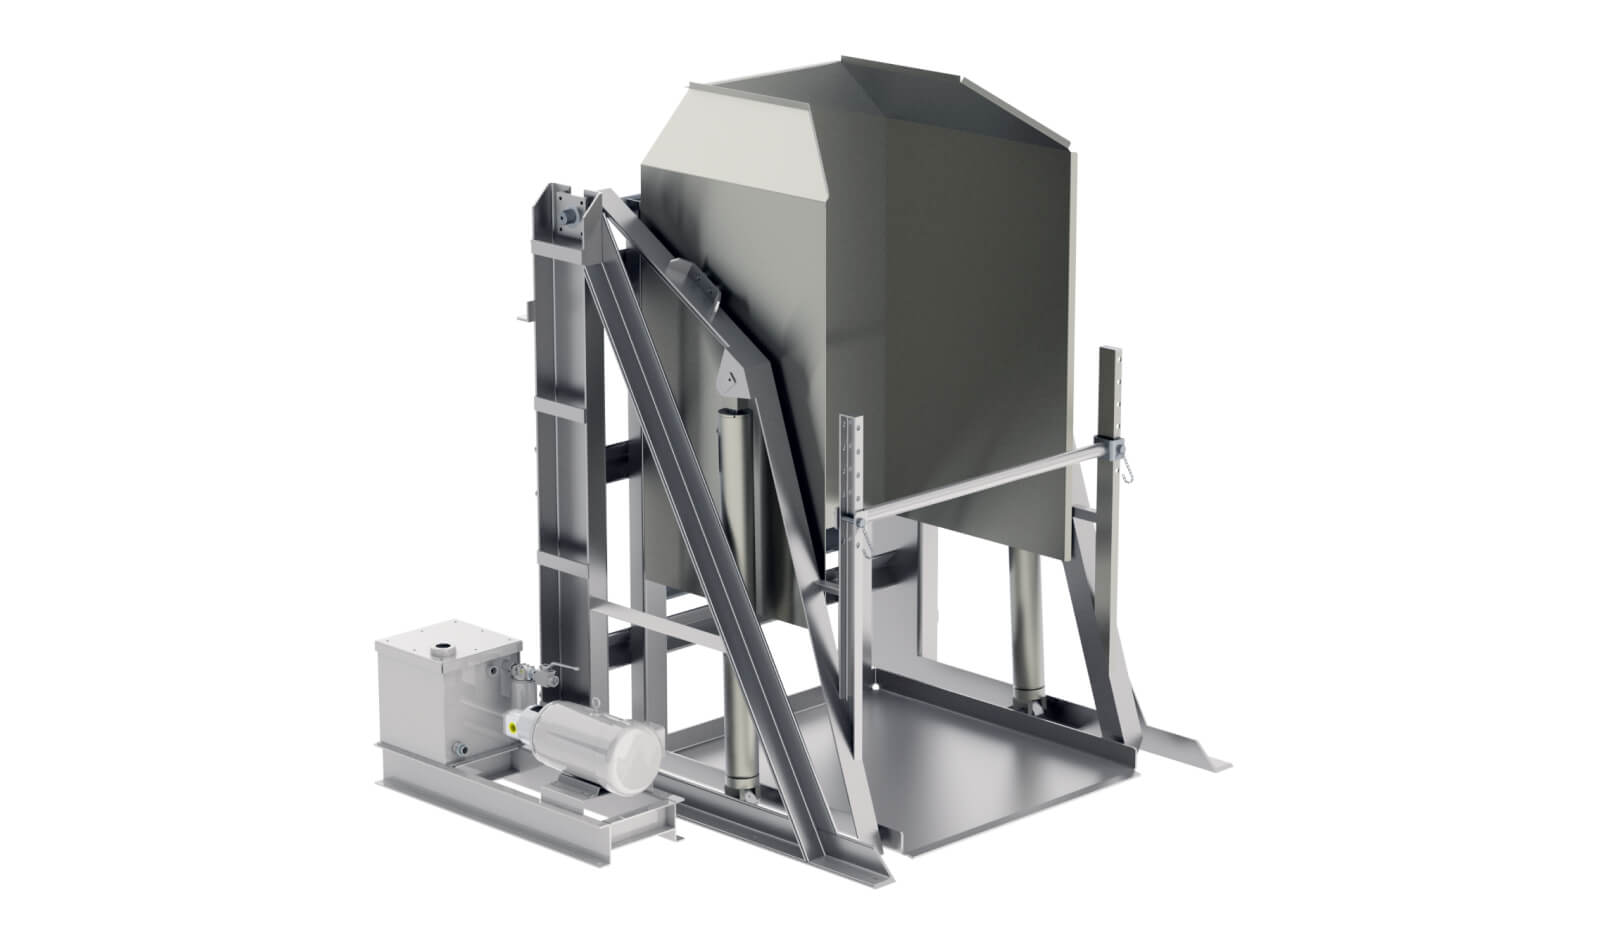
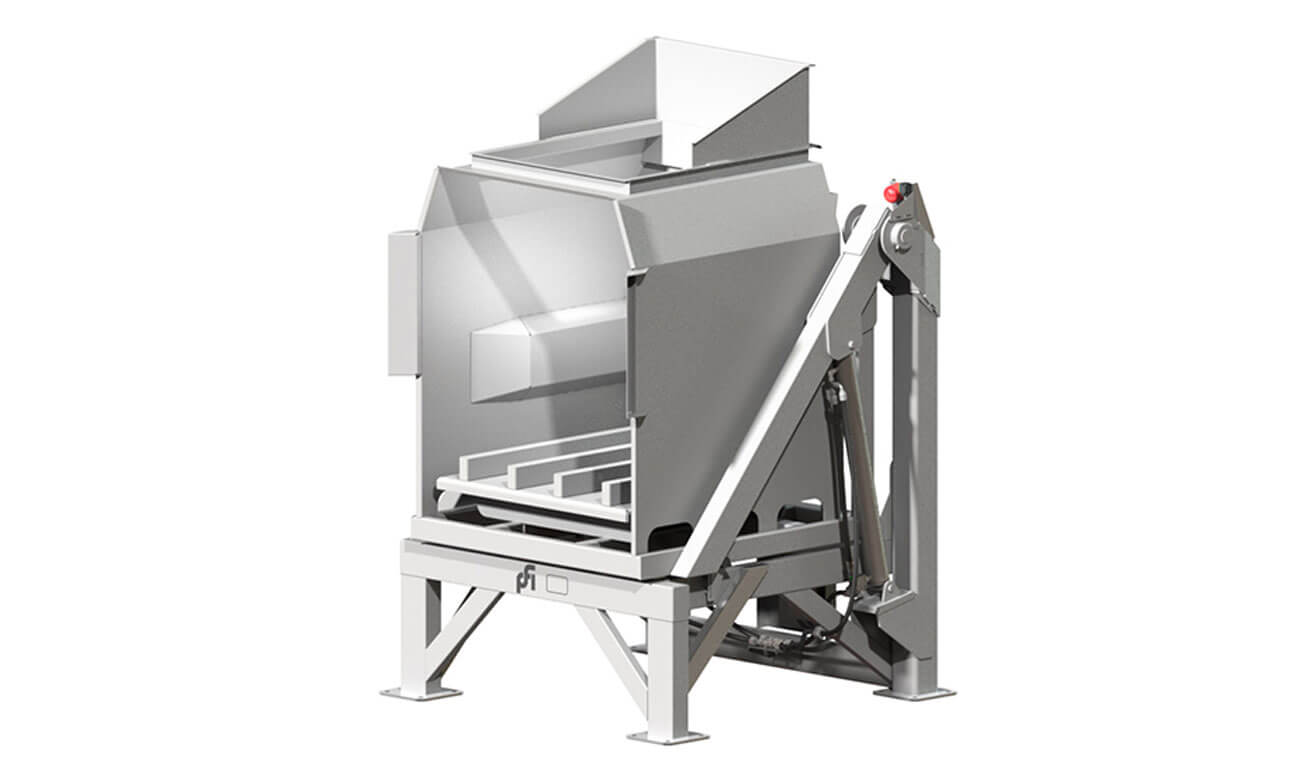
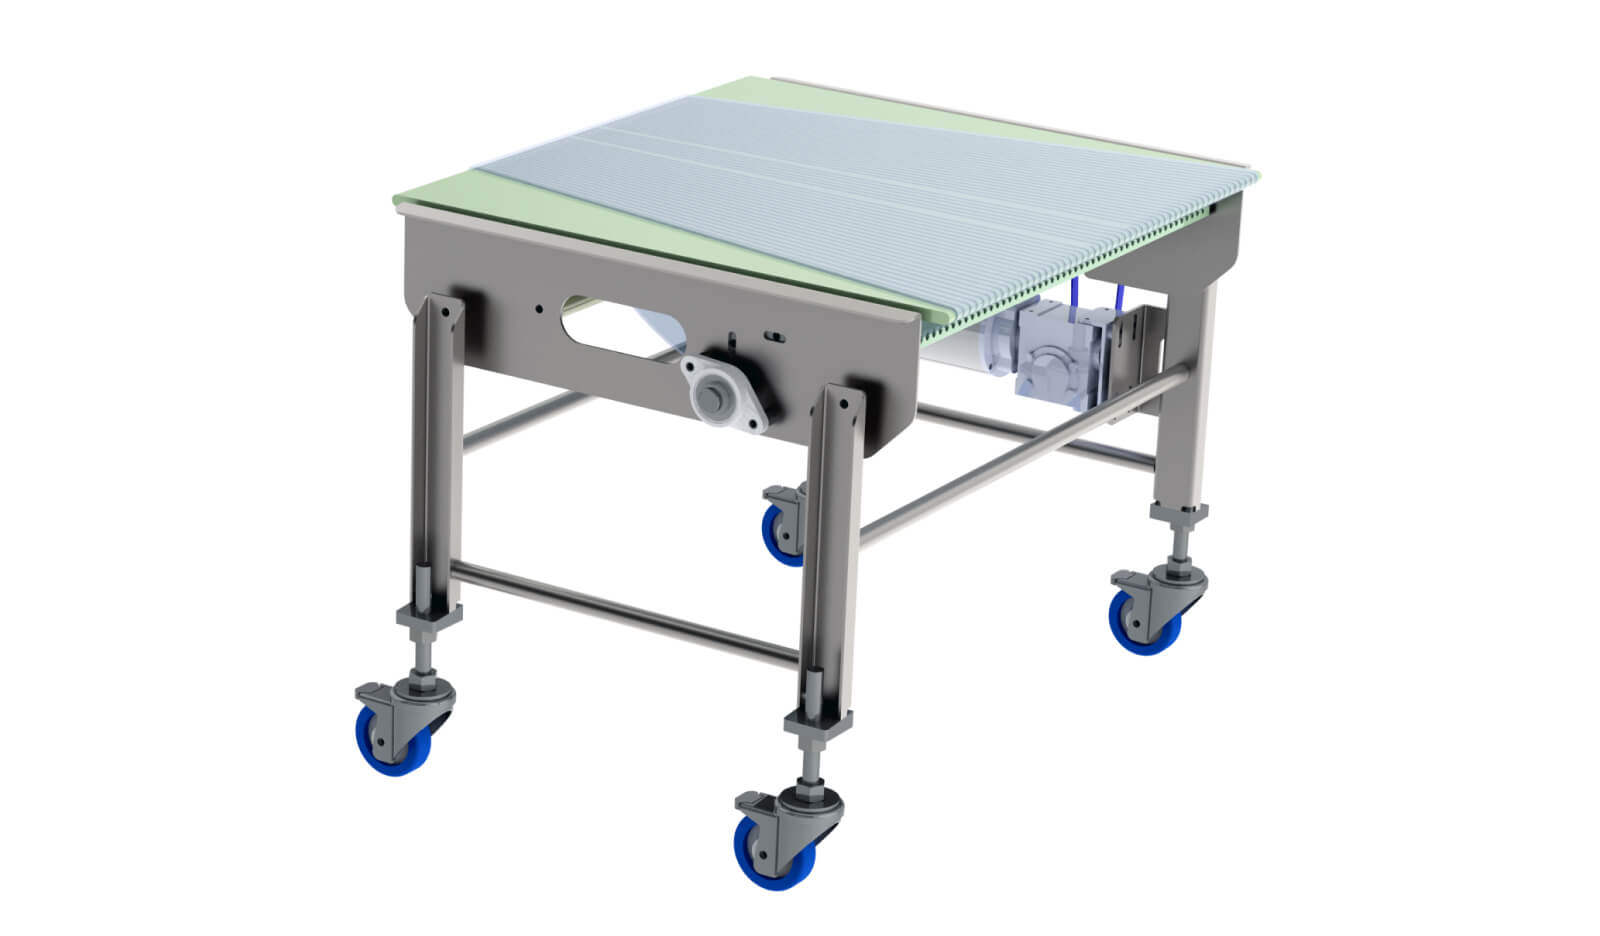
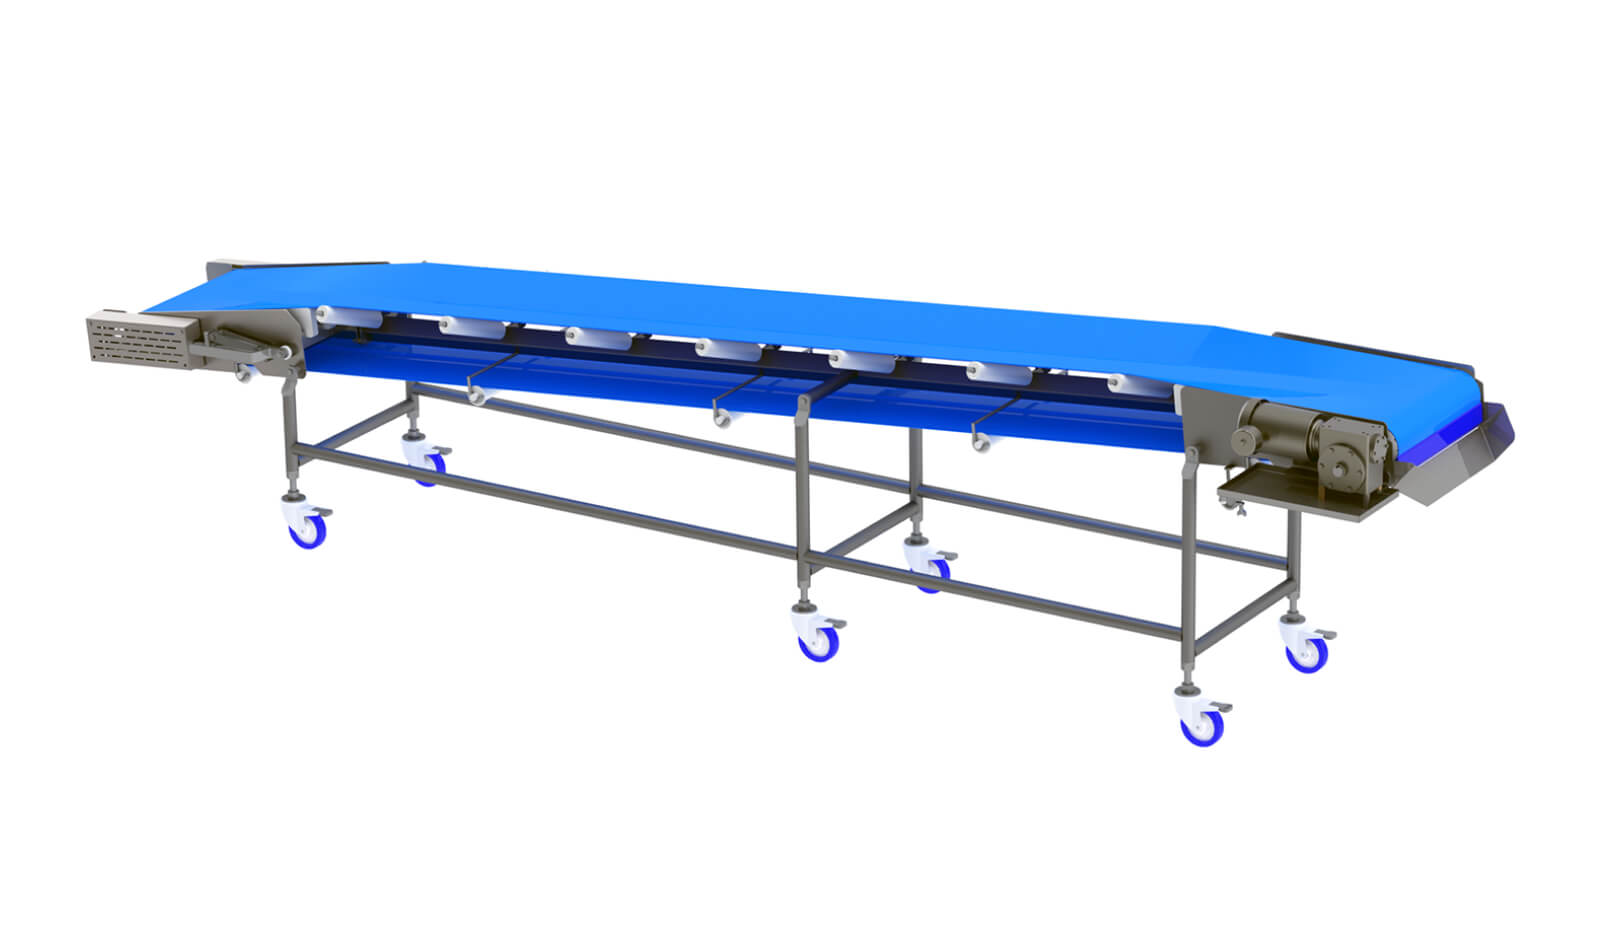
Horizontal Belt Conveyor
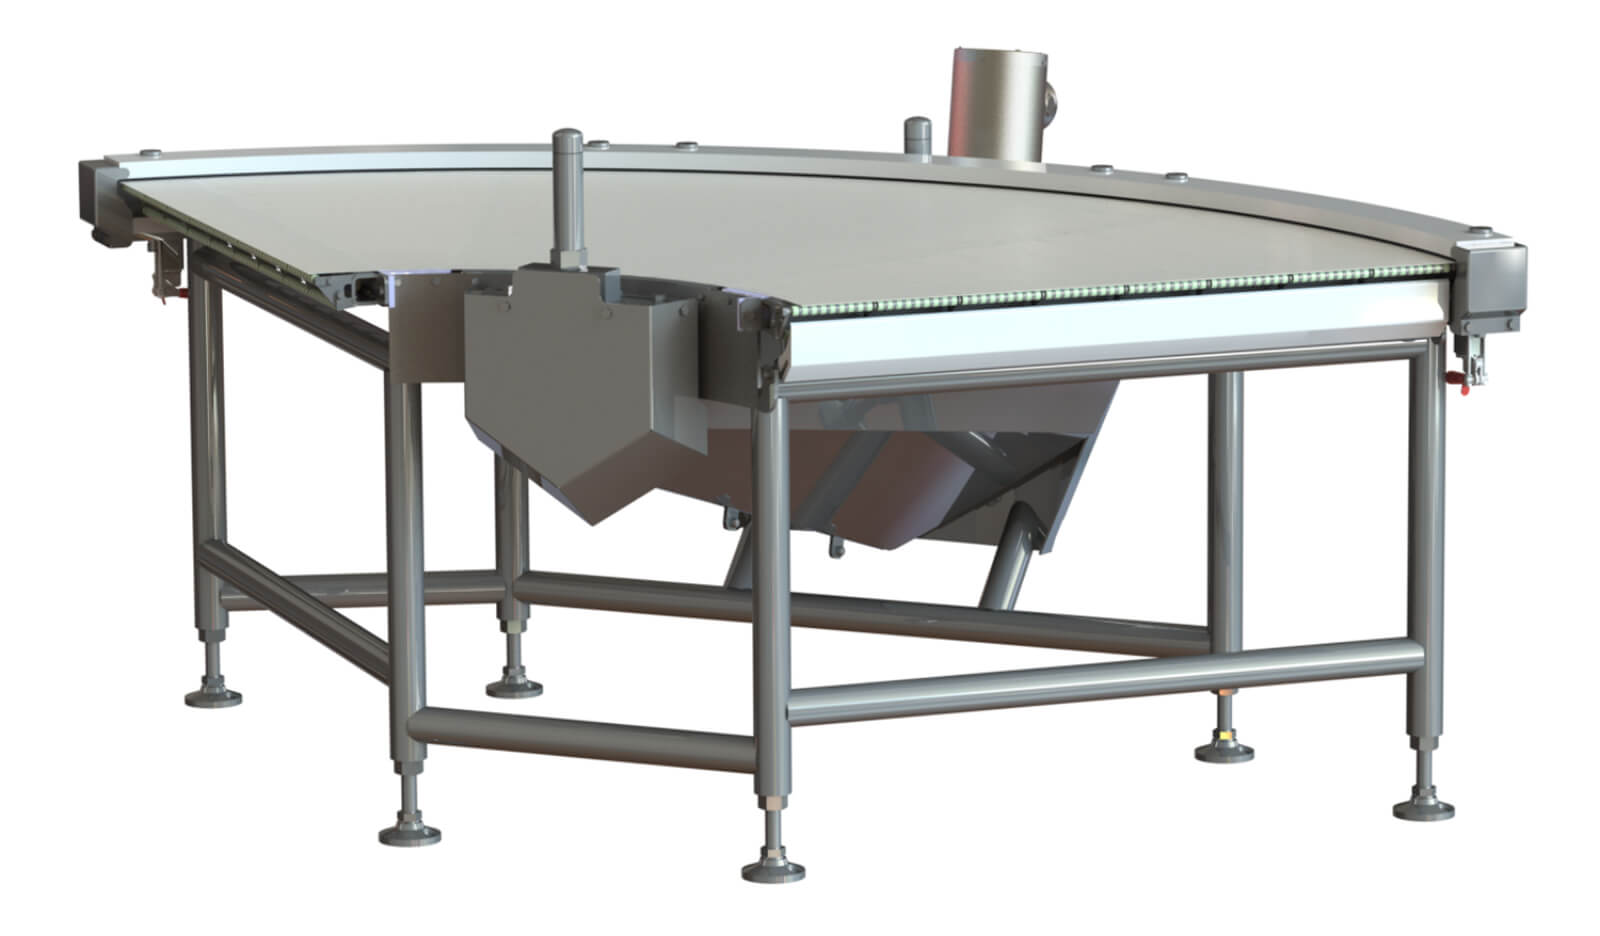
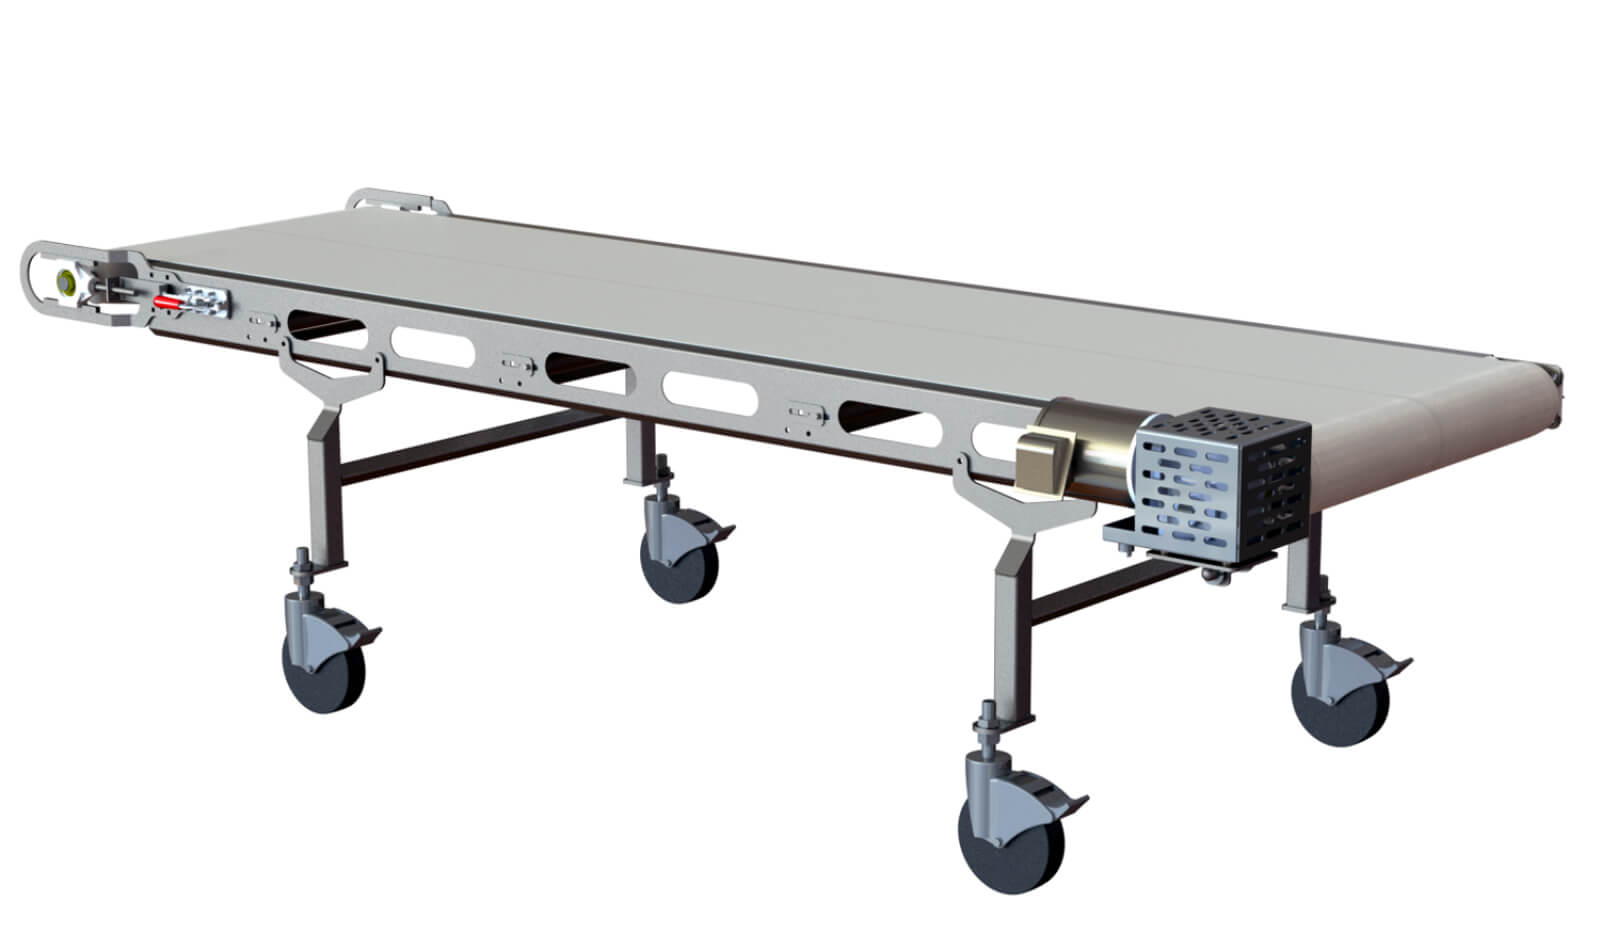
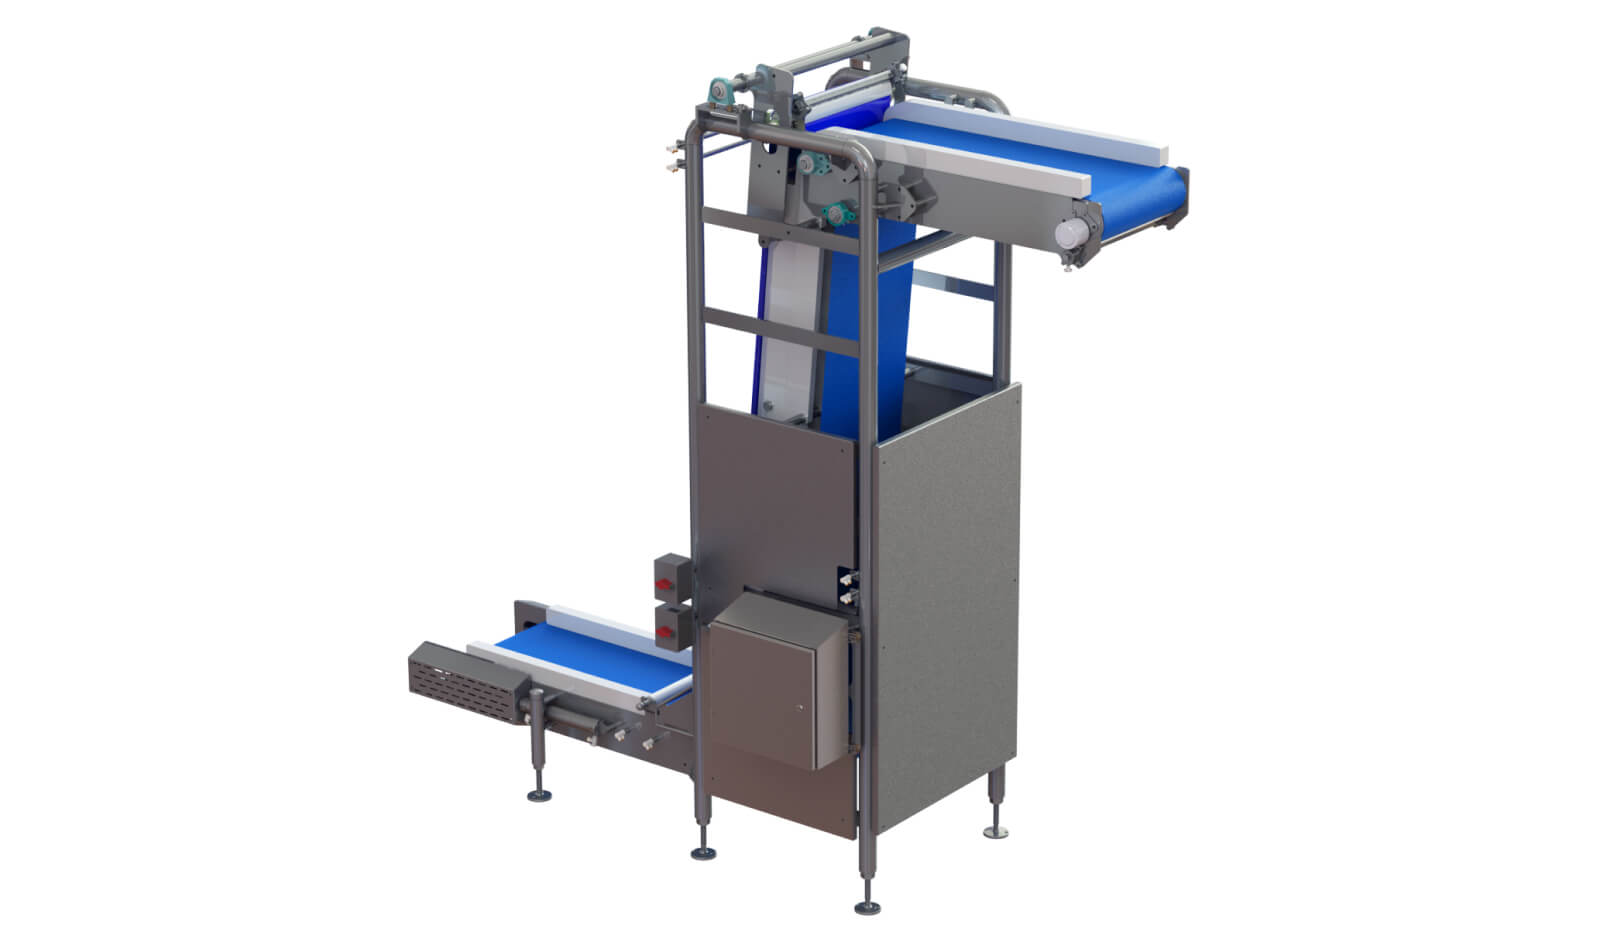
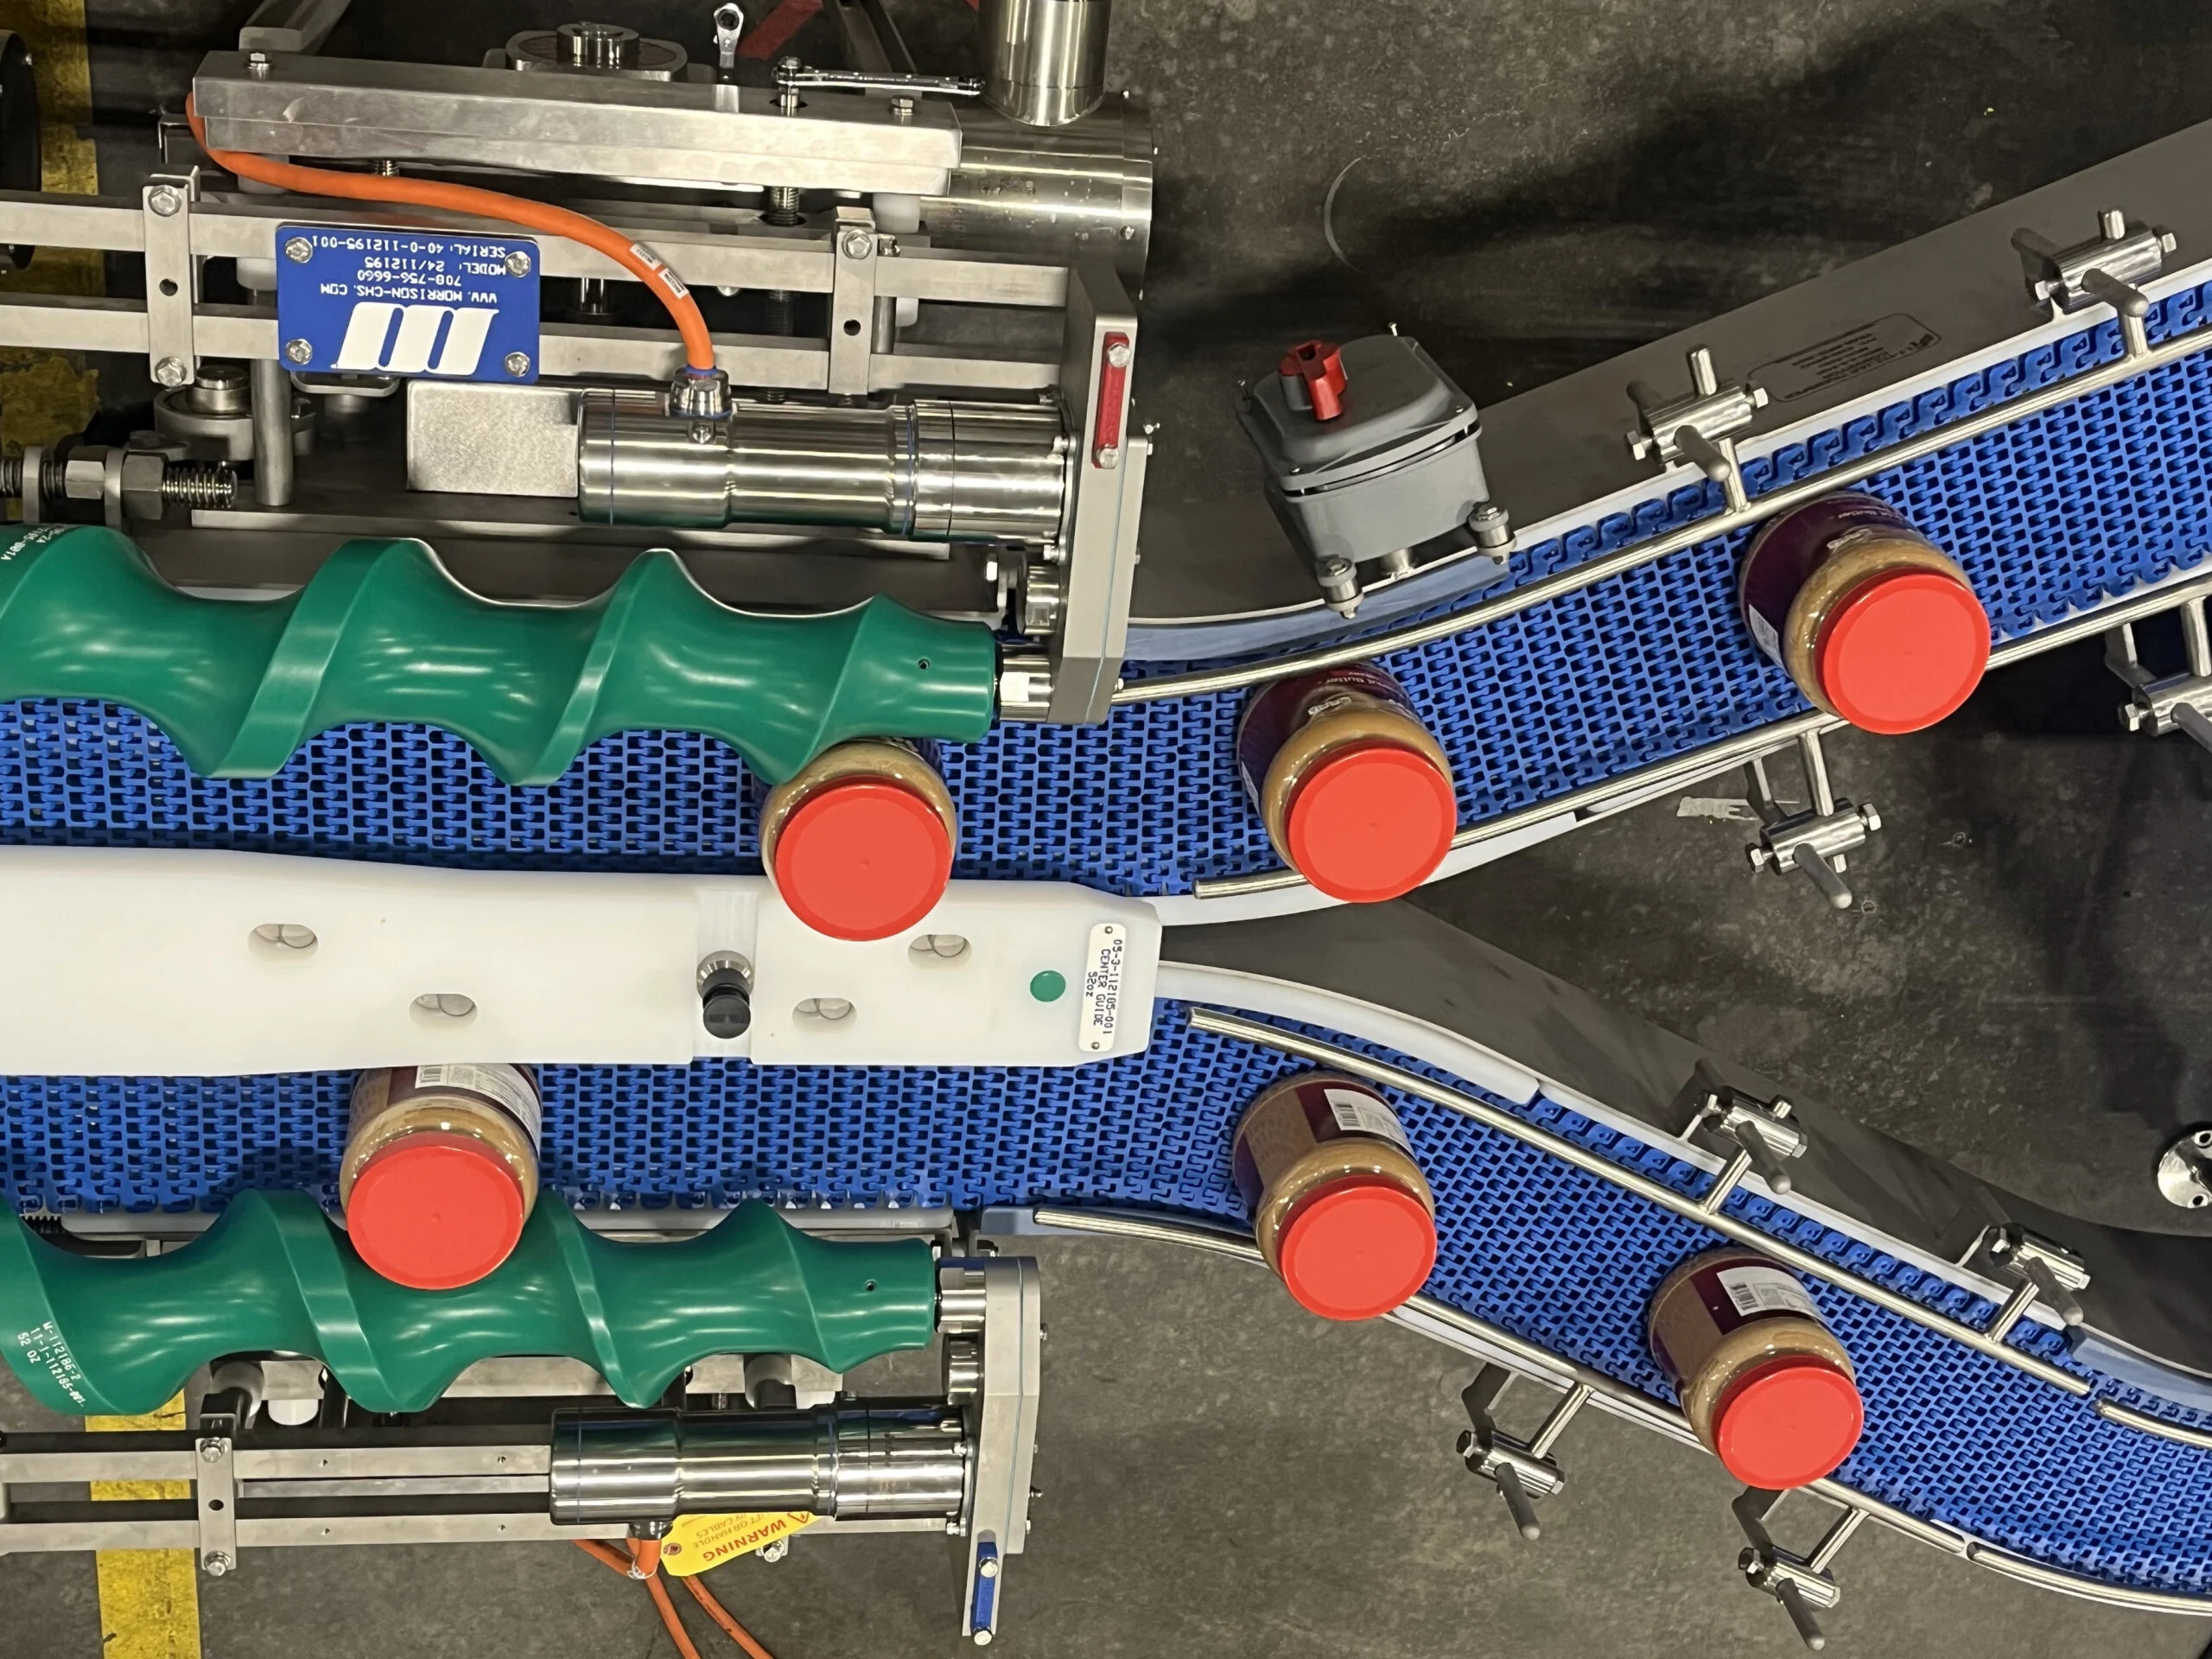
Connect your processing line with flat-bed conveyors built for your exact layout with a range of belt options.
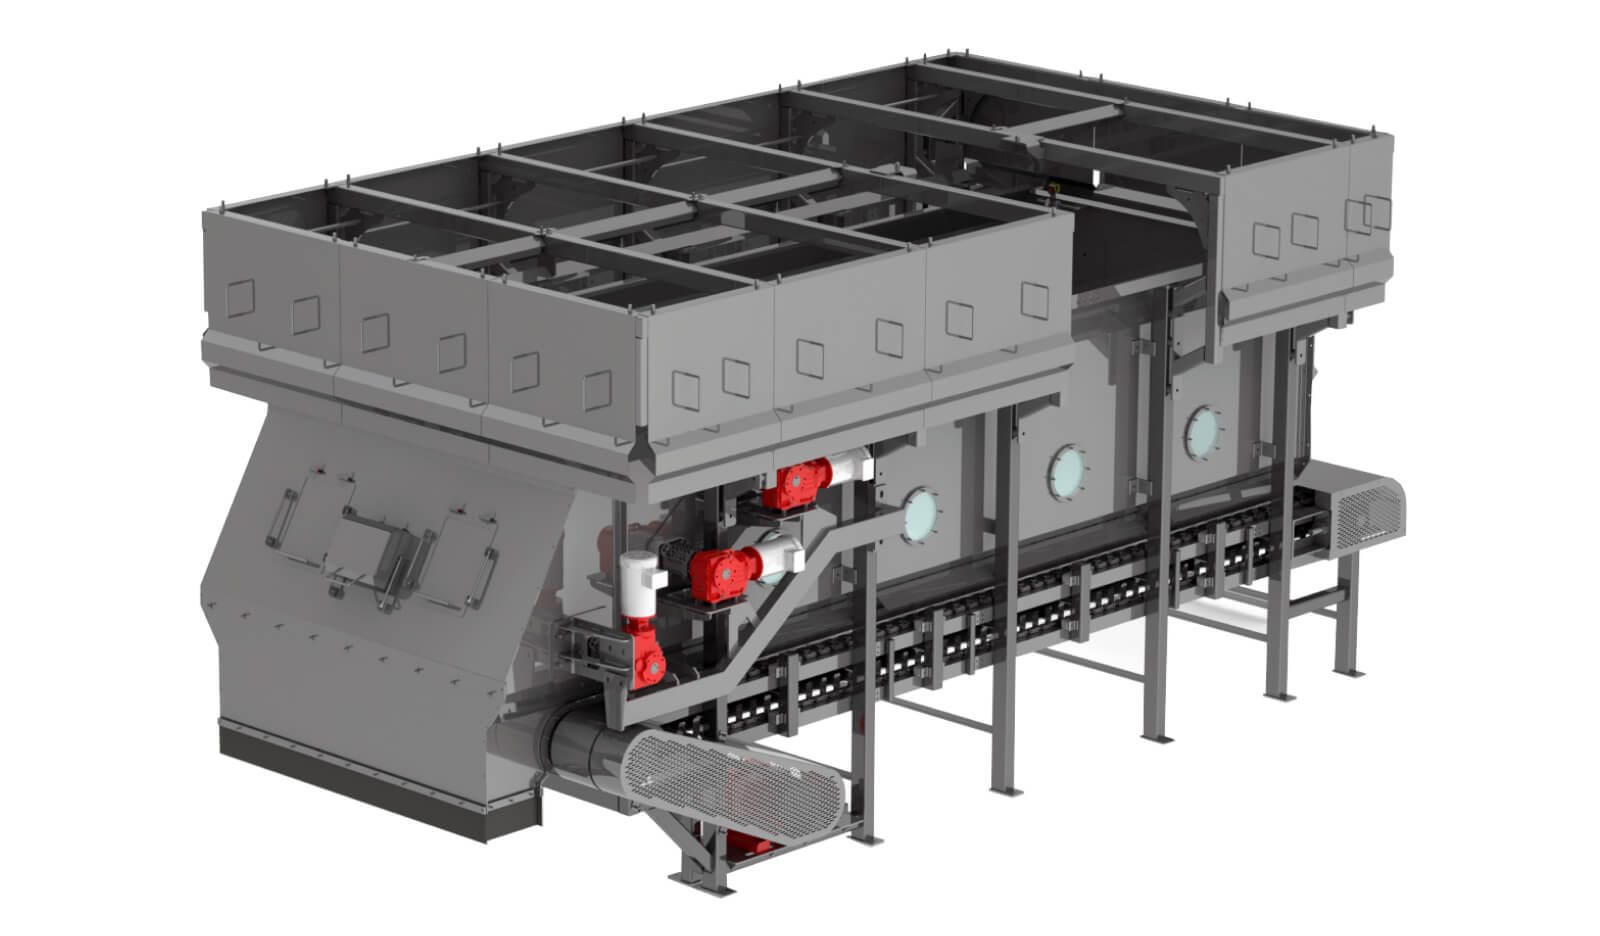
Mix-Blend System
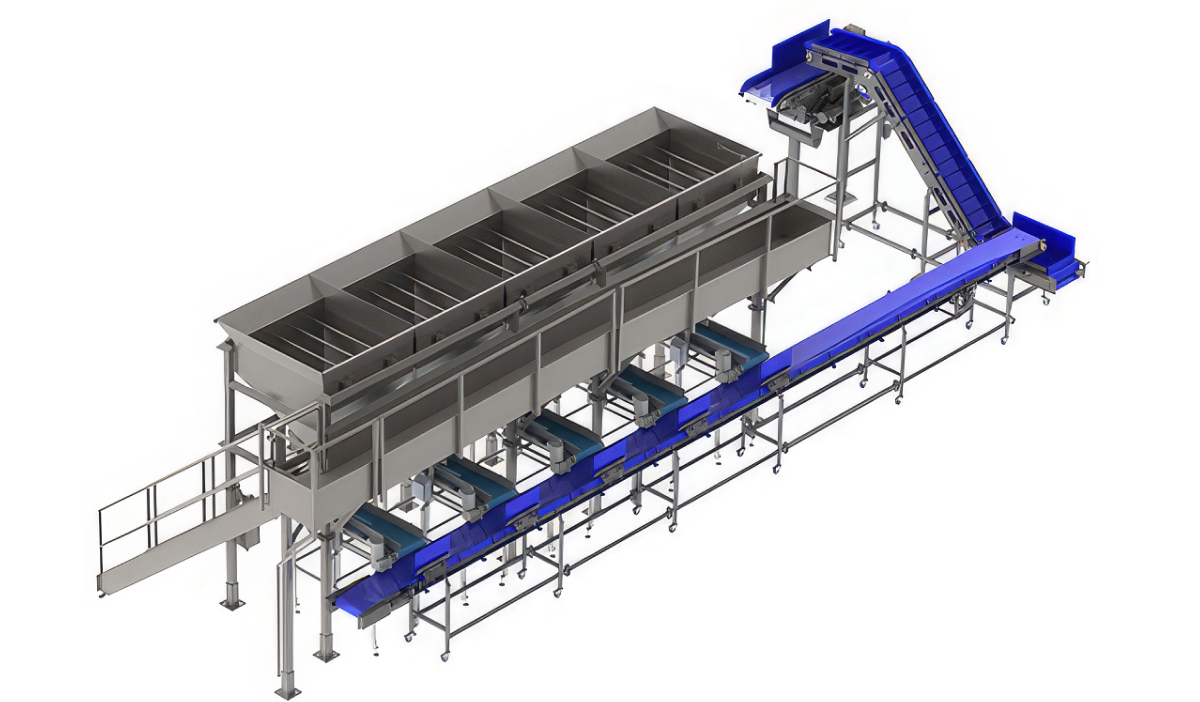
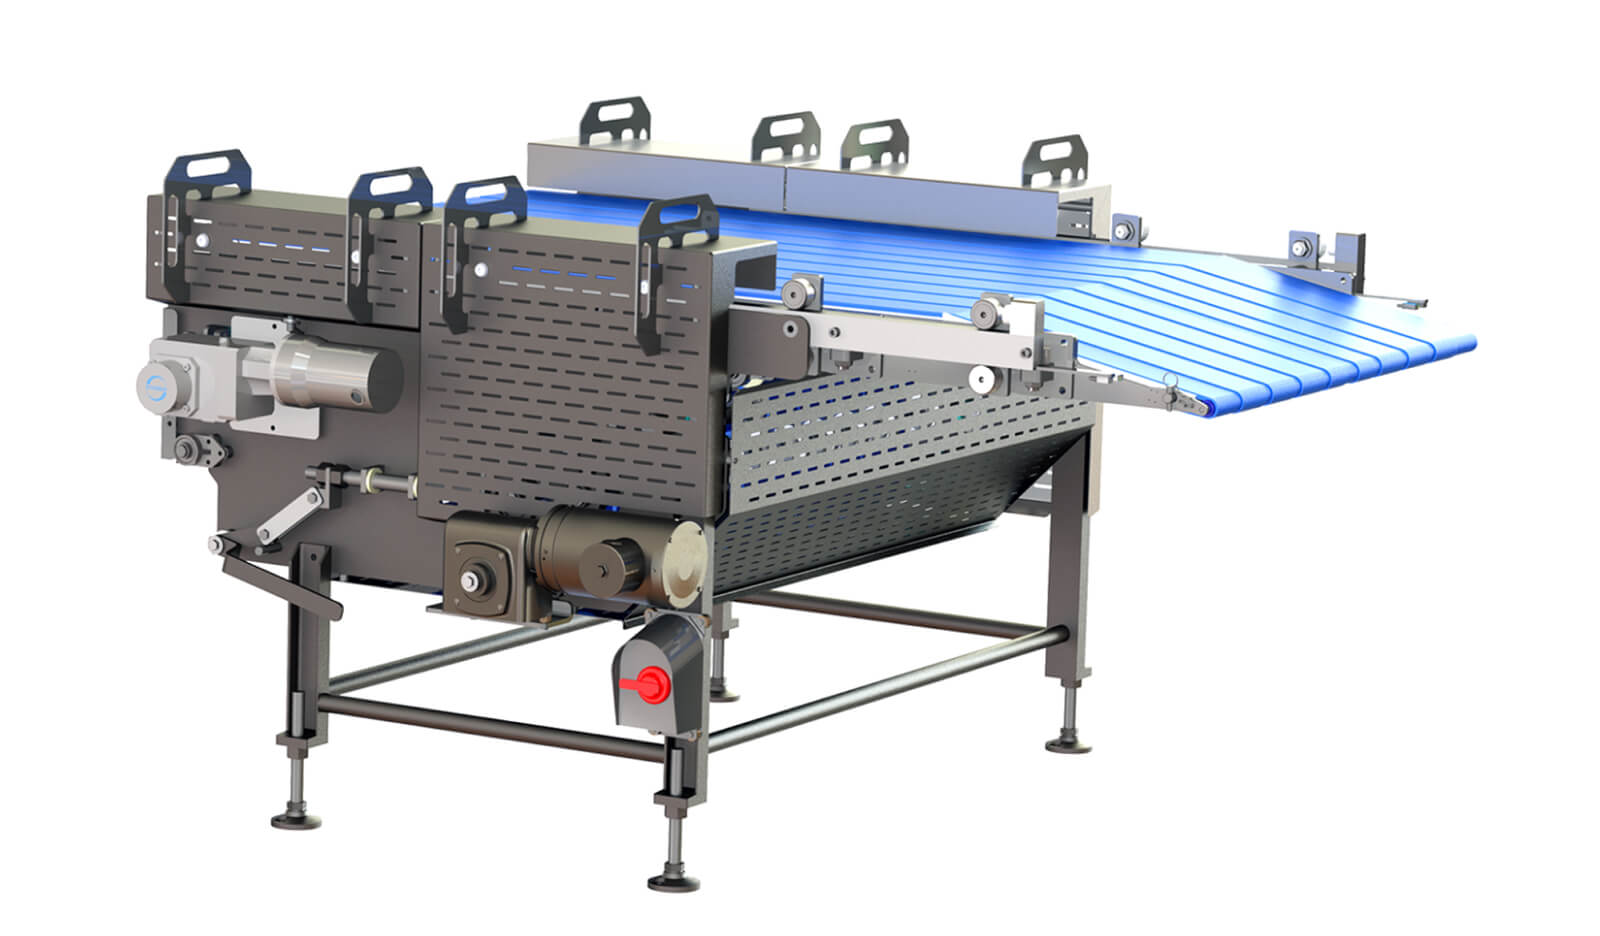
The Mix-Blend System, its components and complementary conveyors give you consistently accurate mixed recipes by feeding multiple products together.
Screw Conveyor
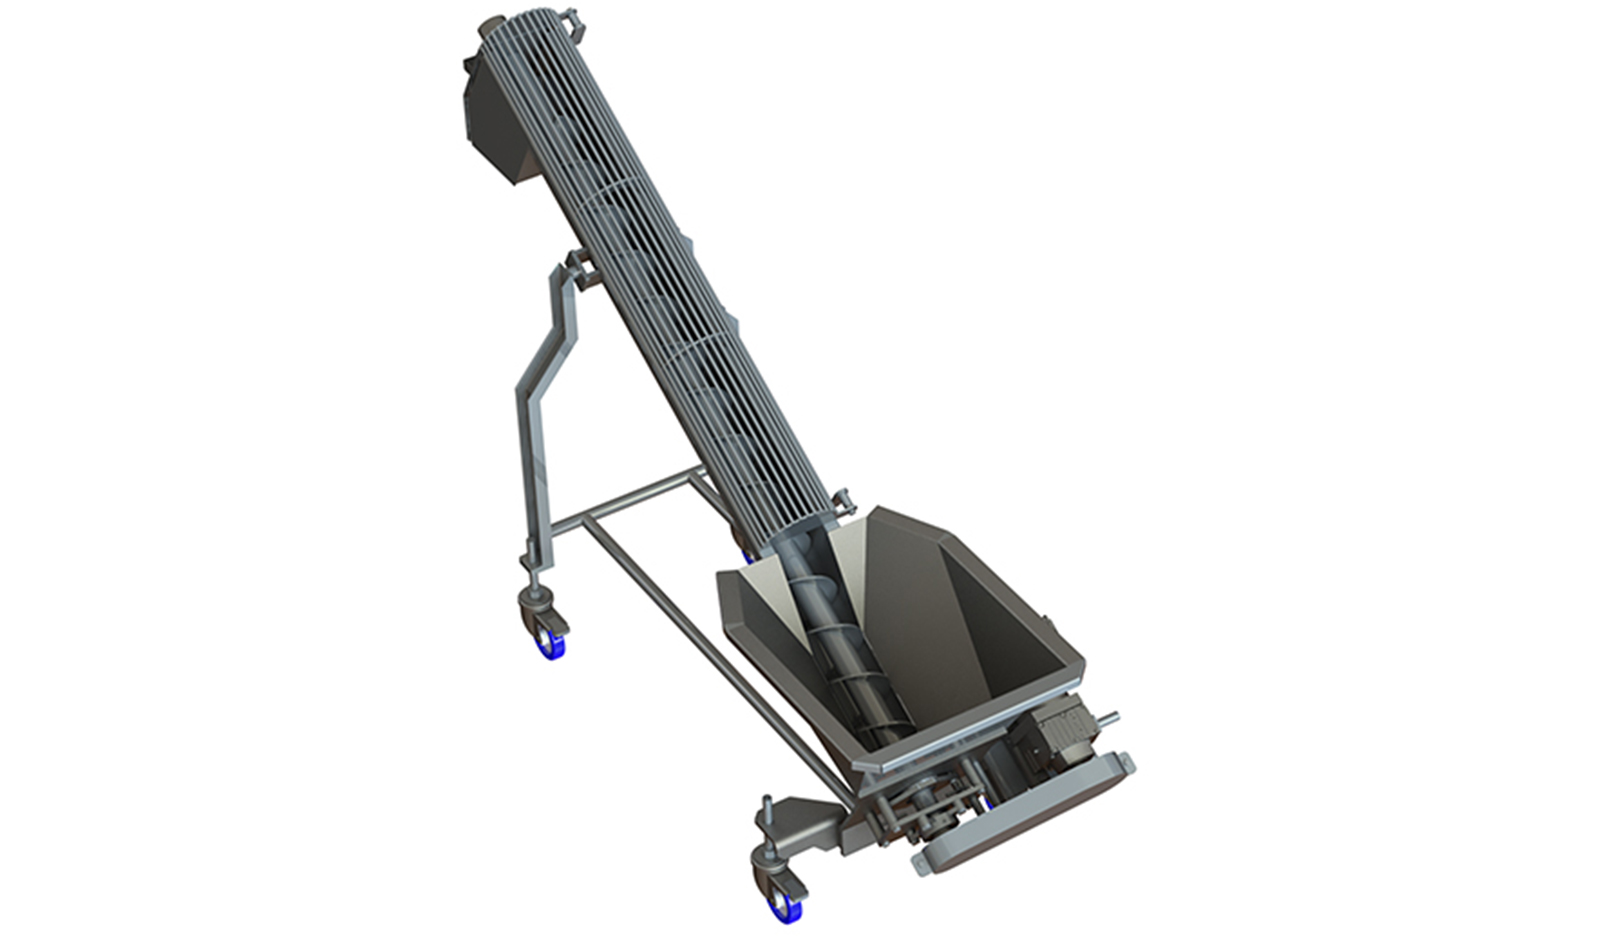
Incline raw and dry bulk food products without spillage or loss. Integrate with dumpers and more throughout your mixing, grinding, and other processes.


REQUEST A CONFIGURATION
Ready to get started on your configuration? Contact us to customize our food-grade sanitary conveying equipment to your application, layout, and processes.

